Skip to content
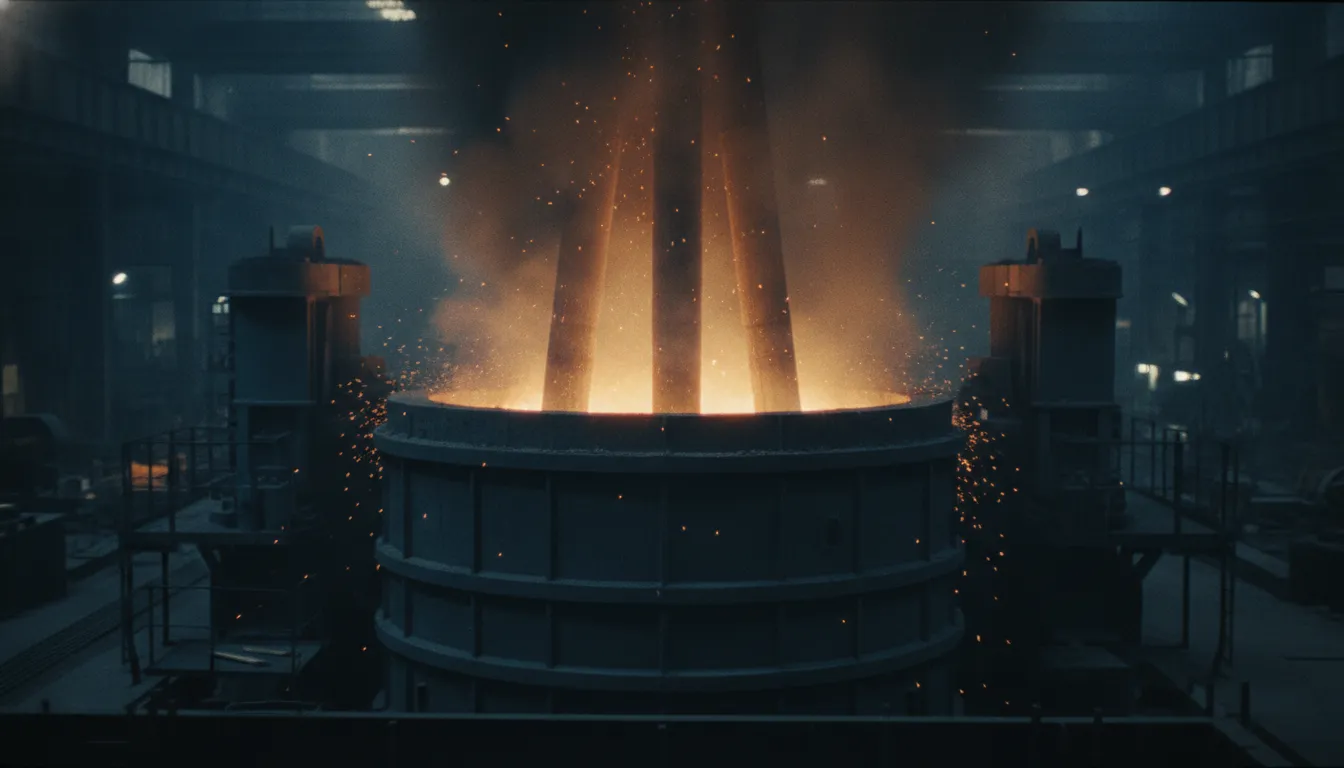
Molten steel being tapped from an electric arc furnace
Home / Facility

Facility and equipment

Below you can see what each line can do, from melting to dispatch. With this information you can check whether your part can be produced at our facility before requesting a quote.

Facility profile

All production takes place at a single site. Parts do not leave for another company between lines.

Location
Kızılpınar OSB, Çerkezköy / Tekirdağ
Covered area
14,500 m²
Open storage yard
9,000 m²
Employees
120
Shift pattern
3 shifts · 6 days a week
Annual forging capacity
30,000 t/year

Production lines and technical specifications

The limits given for each line show the largest part that can be processed on that line. For sizes close to a limit, our team checks suitability separately.

01

Melting and casting

Scrap and alloying elements are melted in the electric arc furnace. The melt is brought to the target chemistry in the ladle furnace and cast into ingot moulds.

Electric arc furnace
30 t/heat
Ladle furnace
Yes · 30 t
Vacuum degassing
Yes (VD)
Ingot weight
2 – 25 t
02

Reheating furnaces

Ingots and intermediate products are heated evenly to forging temperature. The temperature of every furnace is recorded.

Number of furnaces
4
Max. temperature
1,280 °C
Chamber size
6 × 3 × 2.5 m
Fuel
Natural gas · regenerative burners
03

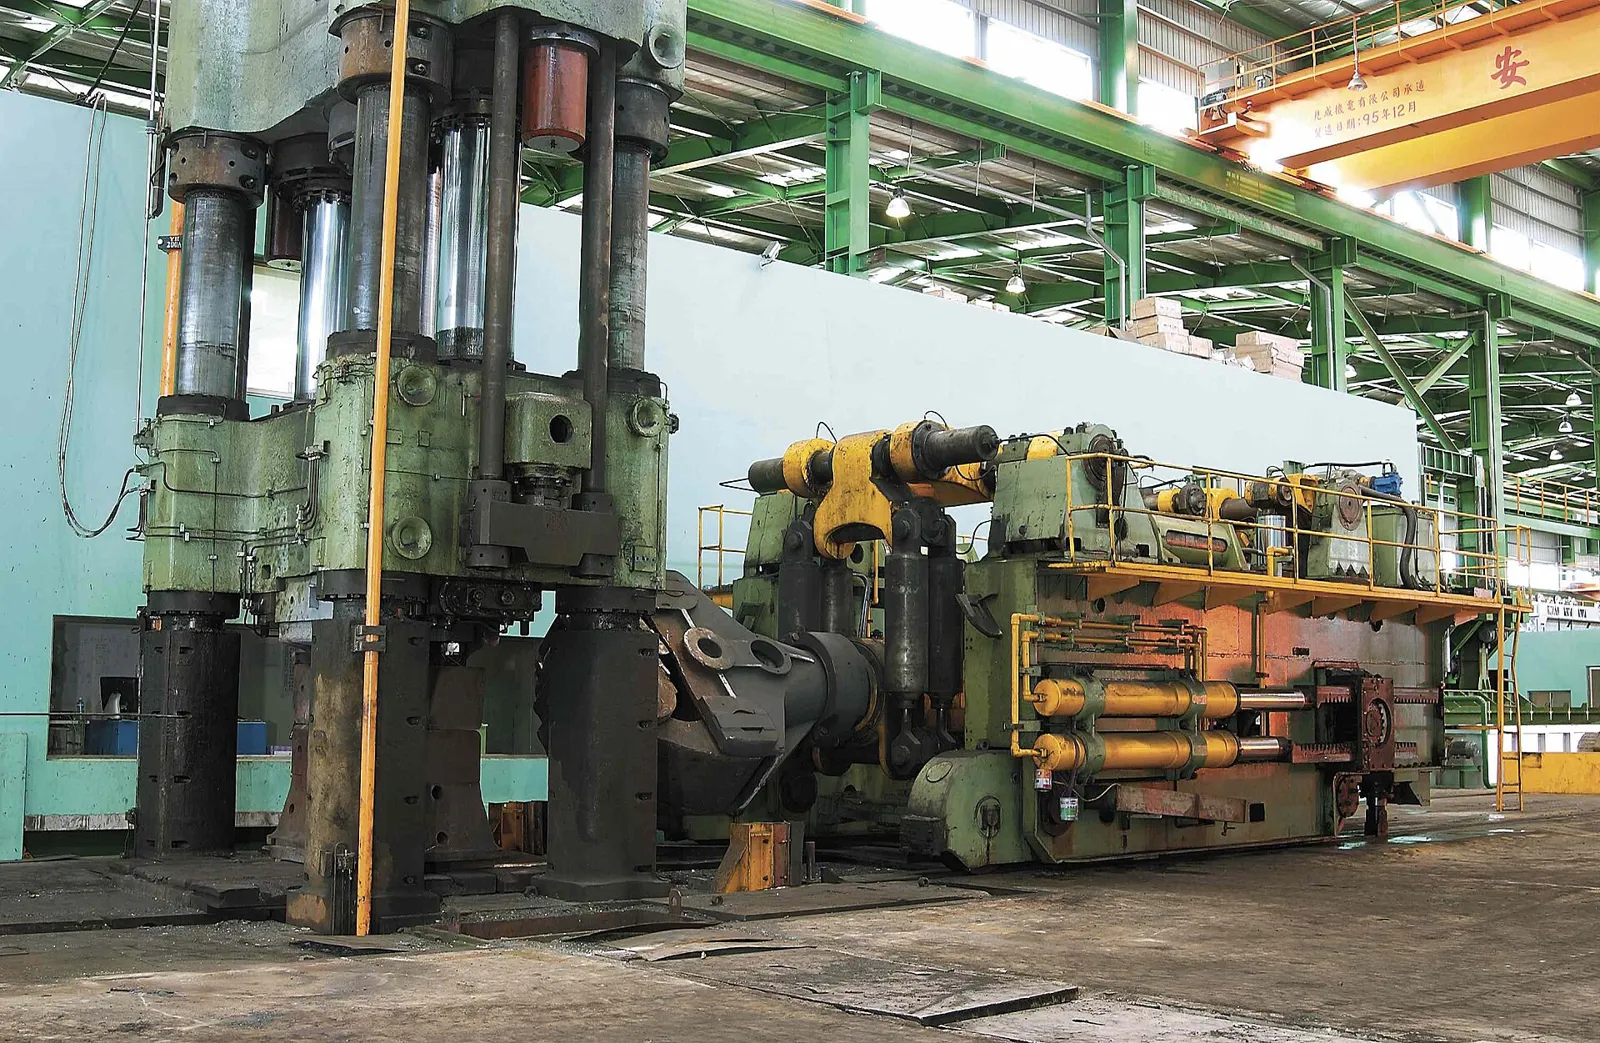
Open-die forging press

On the hydraulic press the ingot is drawn out, upset and brought to the target section. A rail-mounted manipulator turns and feeds the ingot.

Press force
3,150 t
Manipulator
20 t · 50 tm
Max. shaft diameter
Ø900 mm
Max. shaft length
8,000 mm
04

Heat treatment

Normalising, quenching and tempering (water or oil quench followed by tempering) and soft annealing are carried out. Every treatment is recorded against the part's heat number.

Furnace volume
2 × (8 × 3 × 2.5 m)
Water quench tank
220 m³
Oil quench tank
150 m³
Max. part
25 t · 8,000 mm length
05

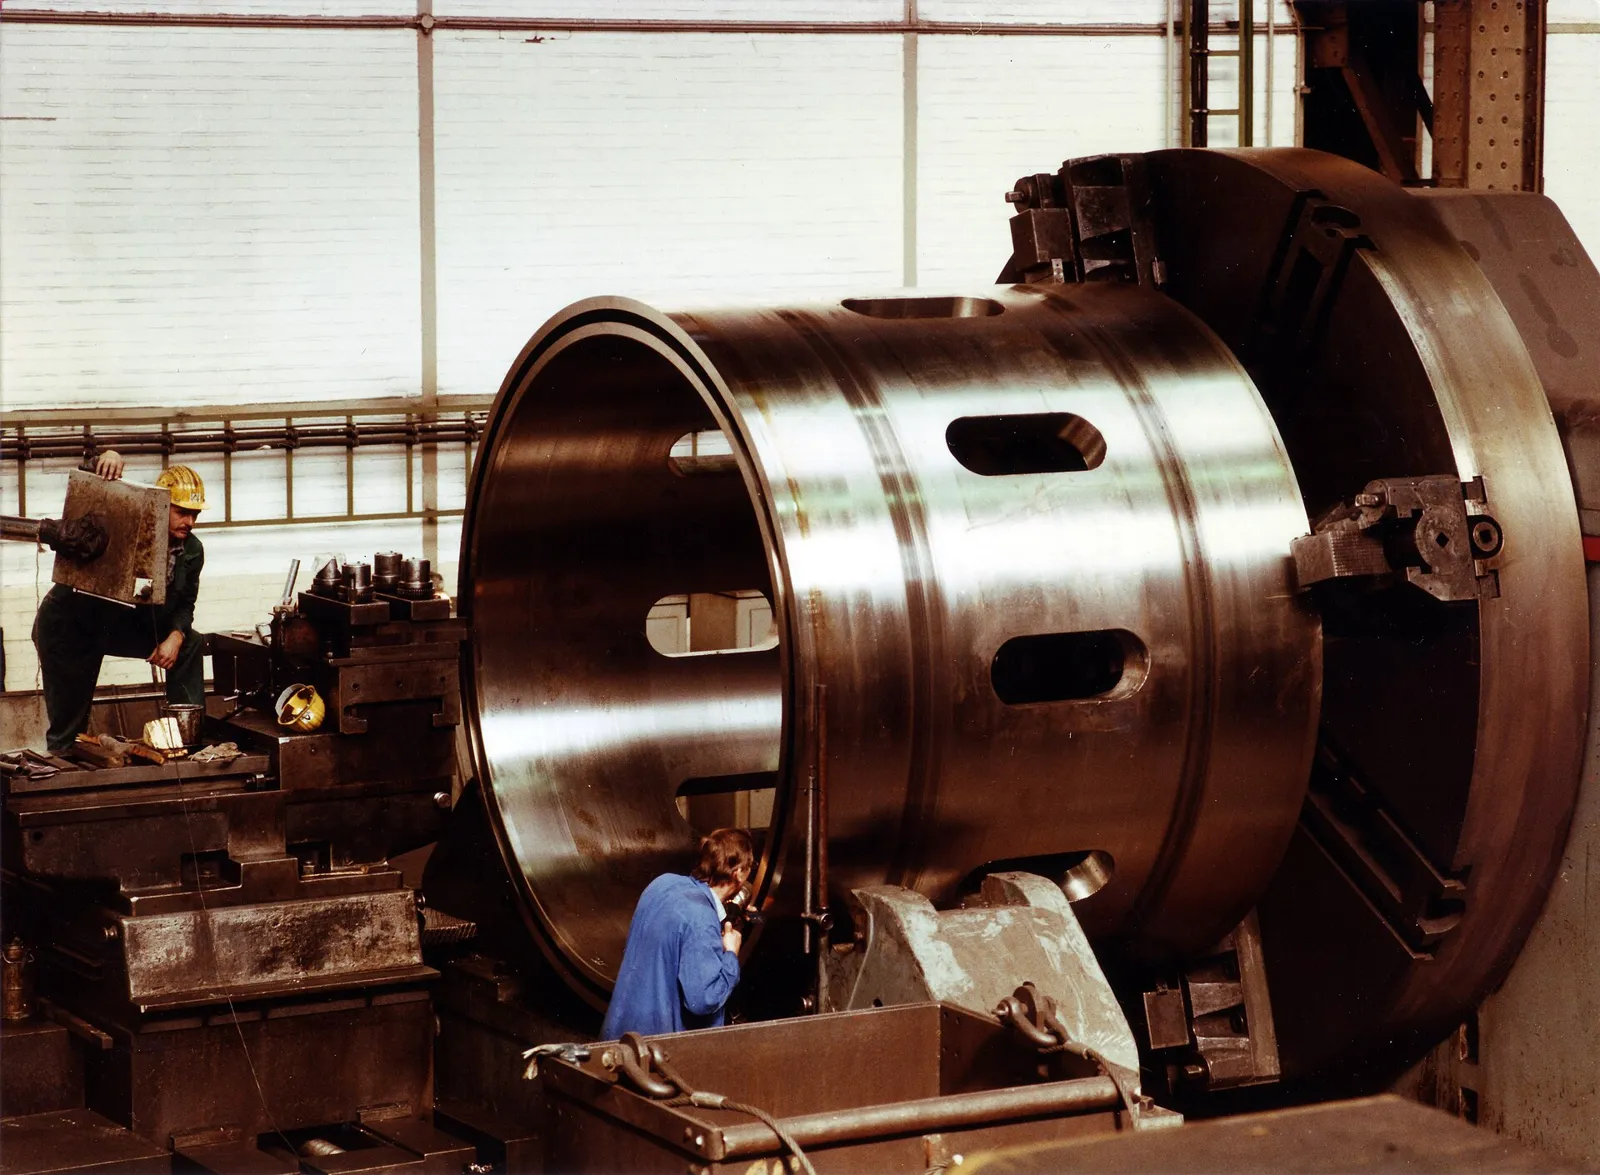
Peeling and machining

The forged scale is peeled off and surface defects are removed. On request, the part is rough turned to the drawing.

Heavy-duty lathe
Ø1,250 × 10,000 mm · 3 units
CNC lathe
Ø600 × 3,000 mm
Milling / machining centre
2,000 × 1,000 × 800 mm
Deep-hole drilling
Ø40 – Ø200 mm
06

Cutting

Shafts are cut to the required length and discs to the required thickness. Every part is stamped with its heat number and part number.

Band saw
Max. Ø1,000 mm
Block cutting
1,000 × 1,500 mm
Cutting tolerance
+3 / 0 mm
Stamping
Heat no. · part no.
07

Laboratory and inspection

Analysis, hardness and ultrasonic test results are entered on the EN 10204 certificate.

Spectrometer
Optical emission (OES)
Ultrasonic testing
EN 10228-3 · 3 level 2 personnel
Hardness
Brinell · stationary and portable
Tensile / impact
TÜRKAK-accredited external laboratory
08

Handling and dispatch

Heavy parts are moved with overhead cranes. Shipments are dispatched together with the documentation file.

Overhead cranes
2 × 32 t + 4 × 10 t
Max. shipped part
25 t
Packing
Timber blocks · strapping · VCI corrosion protection
Delivery
EXW · nationwide in Türkiye · FCA for export
Gallery

Photos from the facility

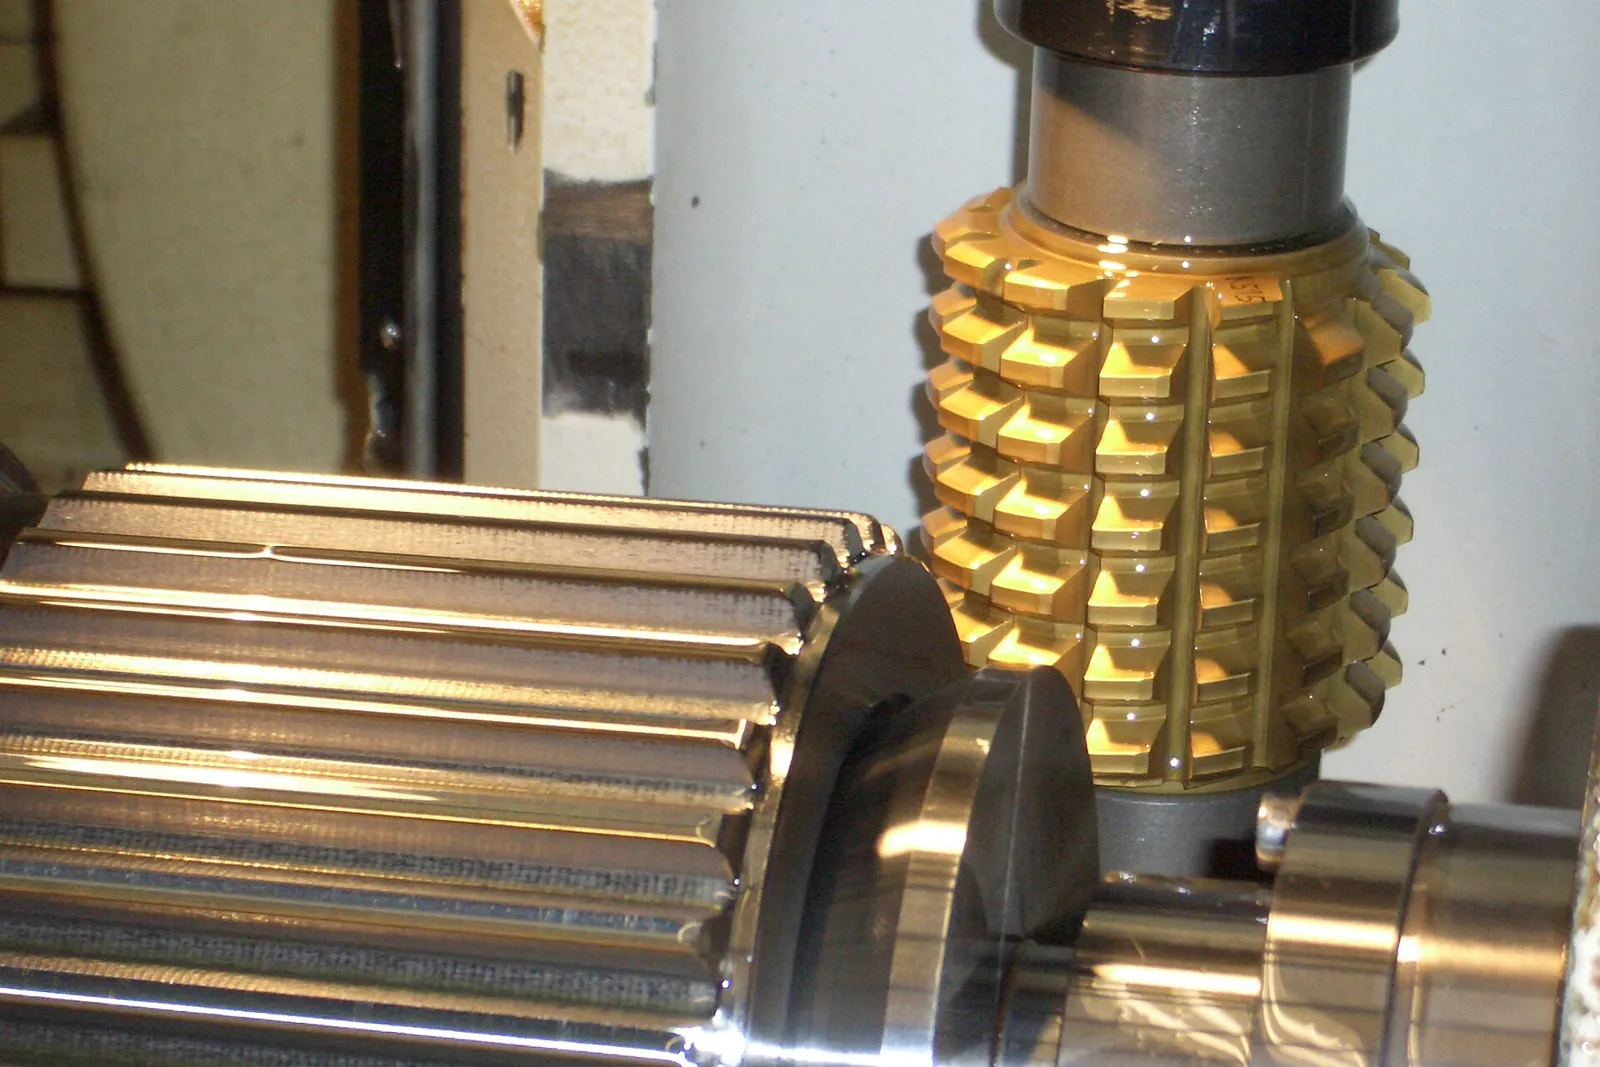
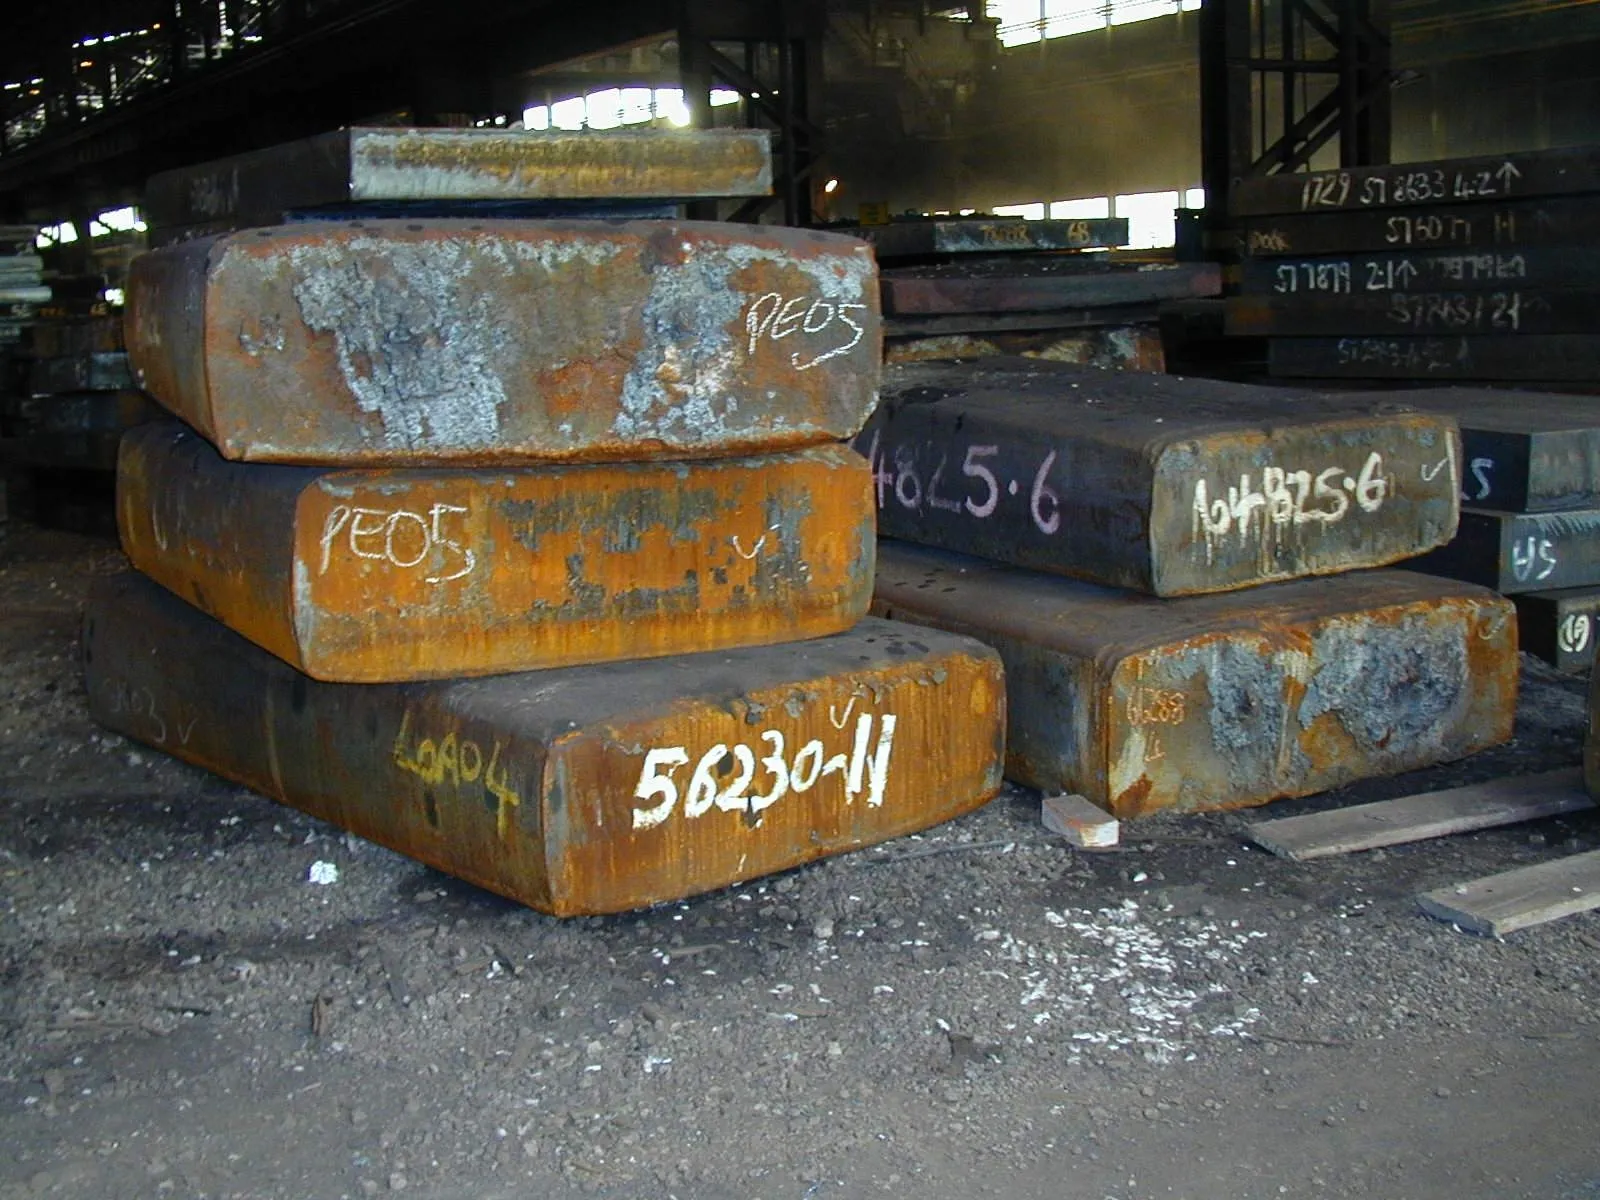
Views of the press, machining and the storage yard.

The photographs are illustrative. Their sources and licences are listed on the image credits page.

Is your part close to the limits? Send us the dimensions and we will review it together.