Home / About us
About us
ASEM Steel produces forged steel shafts, discs and blocks in its own facility, from melting to the finished product.
ASEM Steel produces forged steel shafts, discs and blocks in its own facility, from melting to the finished product.
ASEM was founded in 2023 in Eyüpsultan, Istanbul. Our aim is simple: to deliver the forged steel that gear, shaft and die manufacturers need, in the right size, the right grade and on the day we promised.
The company was founded by engineers and craftsmen with more than 25 years of experience in forging and heat treatment. Our Çerkezköy facility came on stream in early 2024; our first shipment was 42CrMo4 forged shafts for a gearbox manufacturer. Today we supply customers in the energy, mining and die industries on a regular basis.
Forging refines the internal structure of steel and aligns the grain flow with the shape of the part. For this reason, in parts that work under heavy load, impact and fatigue, forged steel does what castings and rolled bar cannot. We do this work with a single focus: large-section, open-die forgings.
The drawing dimensions, machining allowance and tolerance are confirmed in writing before production.
The heat (cast) number is carried on the part and in its certificate from melting to delivery.
Dimensional check and hardness measurement on every part; ultrasonic testing and analysis as ordered.
The delivery date given in the quotation is visible in order tracking; any risk of delay is reported in advance.
Scrap and alloying elements are brought to the target chemistry in an electric arc furnace.
Liquid steel is poured into ingot moulds; each heat is given a heat number.
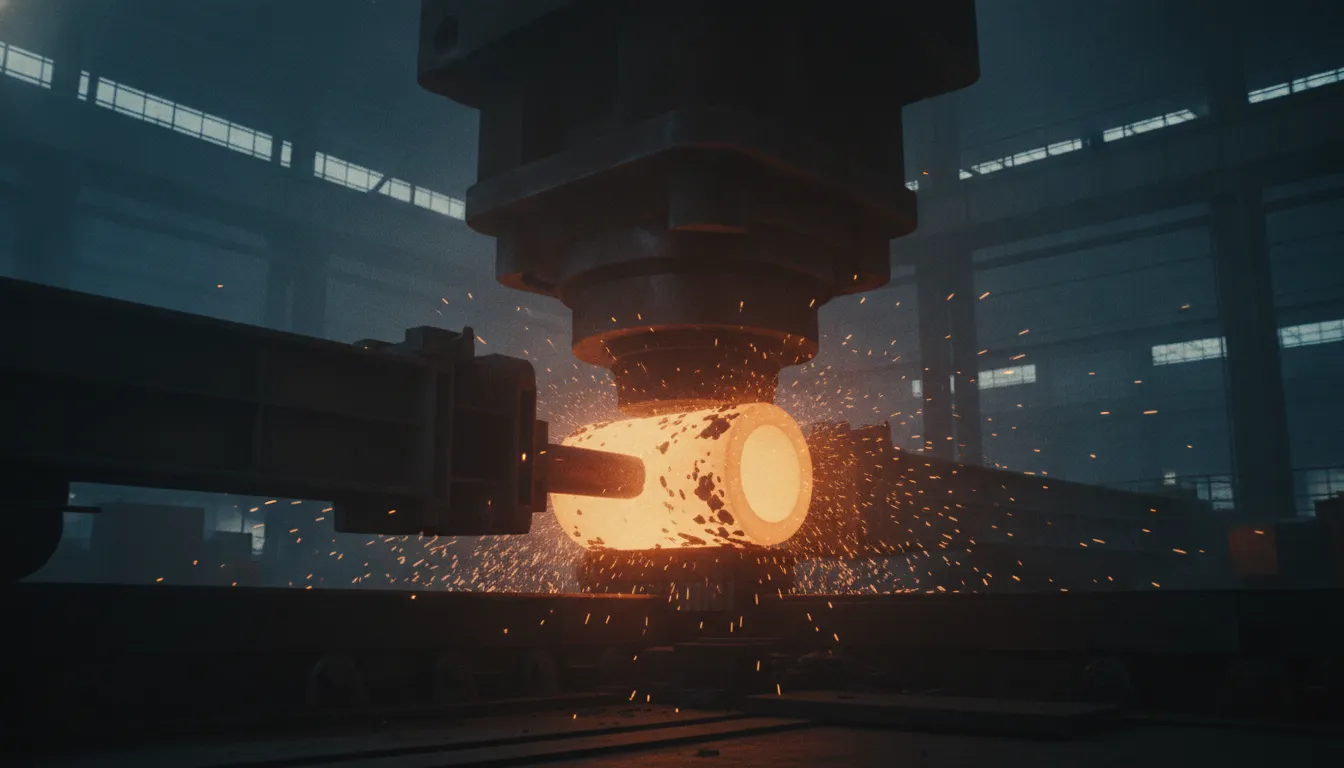
The ingot is heated uniformly to forging temperature (≈1,200 °C).
On the hydraulic press the ingot is drawn out, upset and brought to the target section.
Normalising, quenching and tempering (water/oil quench + tempering) or soft annealing.
The forging scale is peeled off on the lathe and surface defects are removed.
Dimensions, hardness and, as ordered, ultrasonic testing; results are entered in the certificate.
Shafts are cut to the required length and discs to the required thickness, then marked.
Packed and delivered together with the 3.1 inspection certificate.
Special vacuum-degassed grades are bought in as ingots from a contracted steelworks when required. Forging and all later steps are carried out in our own facility.